Factory Enzyme Application Testing Guide
Industrial enzyme selection should not begin with a bulk order. It should begin with a controlled application test that reflects your feedstock, equipment, operating limits, and commercial objectives.
Enzymesproject is an industrial enzyme trial supplier for factories that need a structured path from lab recommendation to production-floor validation. We help process improvement, procurement, and plant operations teams define the trial, control the variables, and measure whether an enzyme is worth scaling.
Wholesale and bulk enquiries. Enzymesproject quotes enzyme supply for manufacturers, processors, distributors and resellers, from trial quantities to repeat bulk orders. Send the product or enzyme class (or the process problem), the quantity you need and the destination country. Pricing, pack sizes and lead time are quoted per order. Request a quote
Why application testing matters before enzyme procurement
The same enzyme category can behave differently across factories because the process conditions are rarely identical. Raw material variation, pH drift, temperature profile, residence time, mixing intensity, hold time, upstream chemistry, and downstream separation constraints can all affect the commercial result.
A supplier recommendation alone is not enough. Before you commit to a production supply agreement, your team needs evidence that the enzyme can perform within your plant’s real limits.
Application testing helps answer practical questions:
- Can the enzyme fit your current process window without disrupting throughput?
- What dosing range produces a measurable benefit without unnecessary cost?
- Which KPI should define success: yield, viscosity, filtration speed, conversion, cleaning burden, reject rate, energy demand, or consistency?
- What operating conditions must be held steady for a valid comparison?
- What risks could appear during scale-up, storage, dosing, or downstream handling?
- Is the improvement large enough to justify procurement, qualification, and implementation effort?
What Enzymesproject provides
We support factories that need more than a product suggestion. Our work is focused on enzyme trial design, application testing, and validation planning for industrial environments.
1. Process-fit review
We start by mapping the current production step where enzyme intervention is being considered. This includes your raw materials, flow path, equipment constraints, operating window, cleaning requirements, batch or continuous format, and key commercial drivers.
The goal is to identify where an enzyme can be tested realistically, not theoretically.
2. Baseline and KPI definition
A valid trial needs a baseline. We help define the comparison point, the measurement plan, and the decision criteria before any dosing begins.
Typical factory KPIs include:
- Yield or recovery improvement
- Cycle time reduction
- Viscosity or flow improvement
- Filtration, pressing, or separation performance
- Conversion consistency
- Reject or rework reduction
- Product quality stability
- Chemical, water, or energy reduction where measurable and process-relevant
- Cleaning frequency or downtime impact
- Cost-in-use versus measured process benefit
We avoid vague success language. Each KPI should be measurable, relevant to the production step, and linked to a commercial decision.
3. Application testing plan
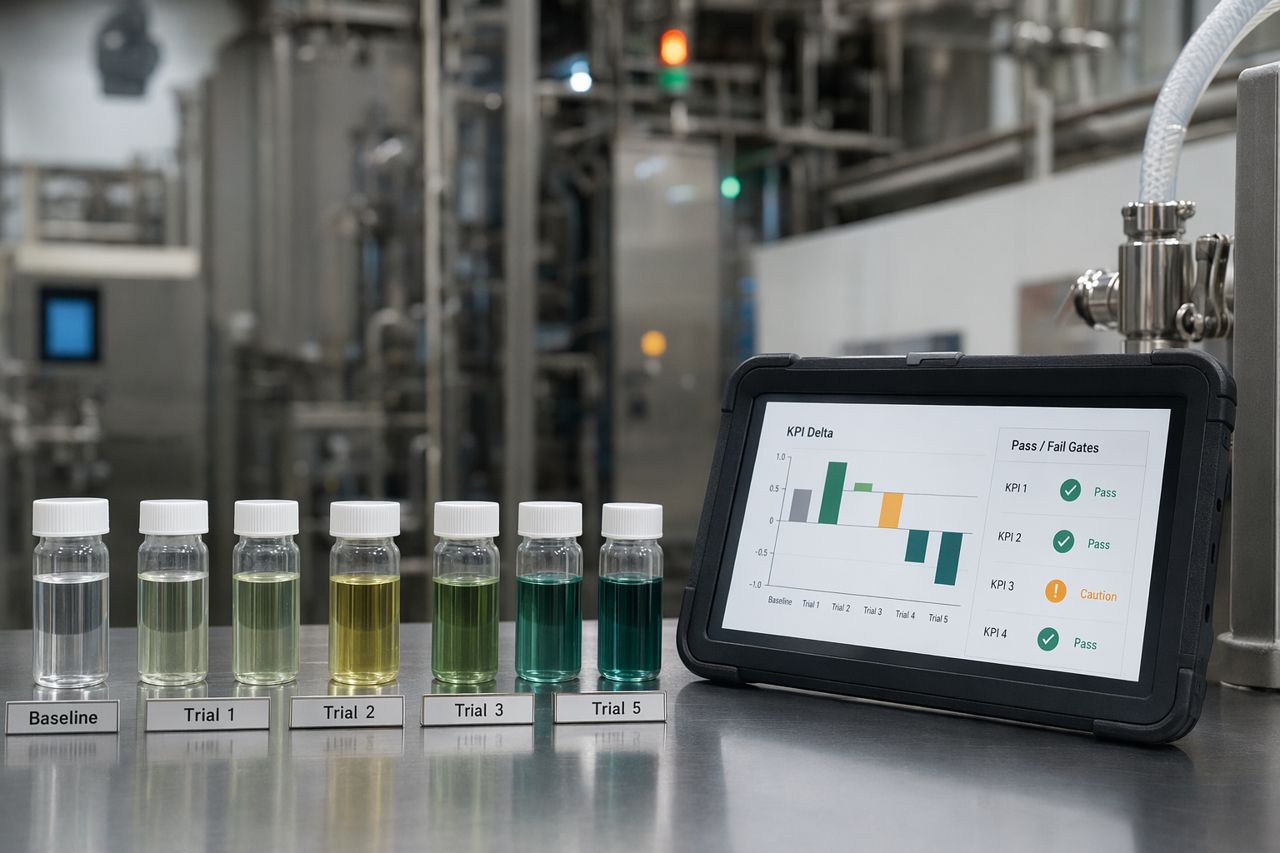
We define a practical test matrix that fits your factory constraints. This may include dosing range, contact time, temperature window, pH window, sampling points, run sequence, hold conditions, and pass/fail gates.
The plan is built to reduce noise and prevent a common problem: running a trial that creates data but not a decision.
4. Enzyme recommendation and trial supply
Based on the application target, we recommend suitable enzyme candidates and provide trial quantities aligned with your test plan. The focus is not maximum complexity. The focus is selecting a controlled shortlist that can be compared under plant-relevant conditions.
5. Production-floor validation support
Lab or bench results are useful only if they translate to your operating environment. We help structure the move from application testing to pilot, extended run, or controlled production validation.
That includes defining scale-up risks, confirming dosing practicality, reviewing data capture, and setting the threshold for procurement approval.
Application testing workflow
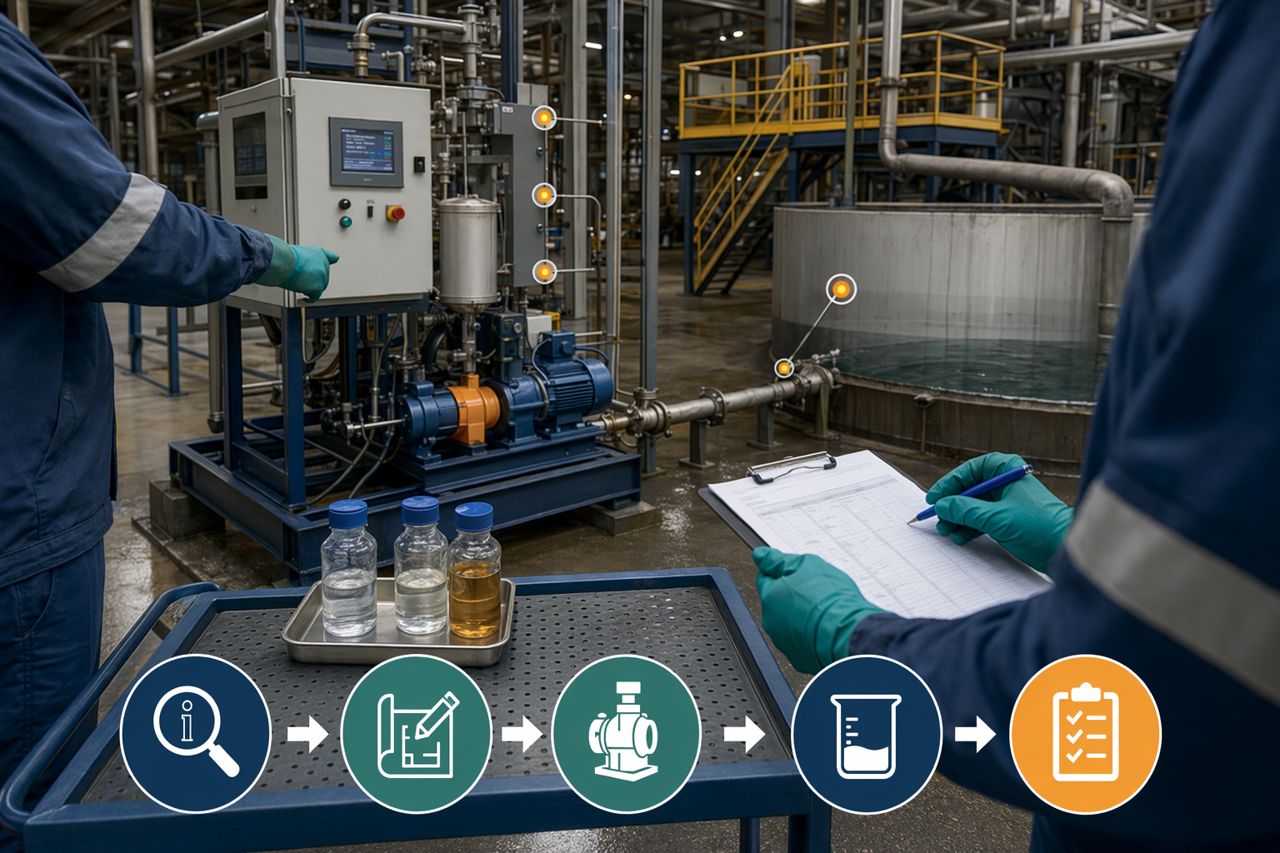
Step 1: Diagnose the process constraint
We identify the production bottleneck or performance gap. Examples include slow separation, inconsistent conversion, high viscosity, excess rework, variable raw material response, or long processing time.
Step 2: Define the enzyme role
An enzyme should have a specific job in the process. We define whether the target is hydrolysis, viscosity modification, release of bound material, conversion support, clarification, cleaning assistance, or another defined technical outcome.
Step 3: Set the trial window
The test must operate inside realistic plant limits. We define acceptable ranges for temperature, pH, contact time, dosing method, mixing, hold time, and any restrictions created by downstream process steps.
Step 4: Build the comparison
We structure the baseline and test runs so that the data is defensible. This includes control runs, sampling timing, repeat points where appropriate, and clear documentation of process conditions.
Step 5: Measure the KPI delta
The trial should show whether the enzyme creates a meaningful shift in the selected KPIs. We focus on the delta that matters commercially, not isolated lab indicators that do not translate to production value.
Step 6: Validate scale-up readiness
If the trial meets the gate criteria, we help define the next step: pilot run, extended production test, supply qualification, dosing equipment review, operator instructions, storage considerations, and procurement readiness.
Where factory enzyme application testing is commonly used
Enzymesproject supports industrial teams evaluating enzymes across production environments where process fit and validation discipline matter.
Common application areas include:
- Food and beverage processing
- Starch, grain, and plant-based processing
- Brewing, fermentation, and distillation operations
- Dairy and protein processing
- Pulp, fiber, and paper-related processing
- Textile wet processing
- Detergent and cleaning process development
- Waste, effluent, and by-product stream improvement
- Feed, rendering, and agricultural processing
- Specialty manufacturing processes involving biological conversion or material modification
Each application is treated as a factory trial, not a generic ingredient substitution.
What a good enzyme trial should control
A reliable application test must control enough variables to make the result meaningful. In many factories, enzyme trials fail not because the enzyme is unsuitable, but because the test structure is too loose.
Critical control points
- Feedstock lot and variability
- Process temperature profile
- pH range and buffering behavior
- Enzyme addition point
- Dosing accuracy and dispersion
- Contact time and residence time
- Mixing or agitation conditions
- Hold time before downstream processing
- Compatibility with other additives or process chemicals
- Cleaning and changeover requirements
- Sampling method and timing
- Operator handling and documentation
Decision gates
A trial should include predefined gates such as:
- Minimum KPI improvement required to proceed
- Maximum acceptable process disruption
- Acceptable cost-in-use range
- Product quality limits
- Operational complexity limit
- Safety, storage, and handling requirements
- Data confidence required before a production test
These gates keep the trial commercially grounded.
Compatibility testing: will the enzyme survive your formula?
In formulated products the choice is rarely enzyme or chemistry. Detergents show it clearly. Surfactants and alkali open up the soil; protease, lipase and amylase then break down the protein, fat and starch that the chemistry alone cannot clear, such as blood, milk and food residues. The smaller fragments are easier for the surfactant to lift and rinse away. When the system is right, the enzyme can allow less surfactant and phosphate and lower wash temperatures.
The same formula can also suppress the enzyme. Strong bleaching agents and harsh alkalinity can cut enzyme activity, which is why detergent makers use protected forms such as encapsulated or alkali-tolerant enzymes. The commercial question is not whether the product contains an enzyme, but whether the enzyme stays active long enough in your system to deliver its value.
Build these checks into the application test:
- Test in the finished formula or the real process liquor, not only in water or buffer
- Run the comparison at your actual use temperature, including the low-temperature settings you want to claim
- Ask for the enzyme form (powder, liquid, granule or encapsulated) that suits how your product is made and stored
What you receive from Enzymesproject
Depending on the project scope, a factory enzyme application testing package may include:
- Process review and application brief
- Trial objective and KPI definition
- Enzyme candidate shortlist
- Trial dosing plan and operating window
- Sampling and data capture plan
- Bench or plant application testing protocol
- Trial supply quantities for controlled evaluation
- Production validation roadmap
- Results interpretation and next-step recommendation
- Procurement support criteria for scale-up decisions
The output is a practical decision framework: proceed, adjust, retest, or stop.
When to request a quote
Request a quote when your team is preparing to evaluate an enzyme before bulk ordering and needs a structured plan rather than a generic recommendation.
You may be ready if:
- You have a defined process step or bottleneck
- You know which KPI needs improvement
- You can provide operating conditions and constraints
- You need trial quantities for a controlled application test
- You need help comparing enzyme candidates
- You need a validation plan before procurement approval
Request a quote
Use the on-site request form to share the product or enzyme class, the trial quantity and expected volume, the destination country, your process target and your trial objective. Manufacturers, formulators, distributors and resellers are welcome. Enzymesproject will reply by email with a quote for trial supply, application testing support and bulk supply after validation.
Request a quote using the contact form
Include where possible:
- Industry and process step
- Current bottleneck or performance target
- Raw material or substrate type
- Operating temperature and pH range
- Batch or continuous process format
- Target KPI and current baseline
- Expected trial timing
- Any plant constraints, handling limits, or procurement requirements
Frequently asked questions
Do we need a complete process dataset before requesting a quote?
No. A concise process brief is enough to begin. We can identify the missing information needed to design a useful trial.
Can you support testing before we choose an enzyme?
Yes. Enzymesproject can help define the application target, shortlist enzyme candidates, and structure the test plan before trial supply is arranged.
Is application testing suitable for an operating factory?
Yes, if the test is designed around plant constraints. We help define a controlled trial that respects production schedules, operator workload, equipment limits, and quality requirements.
What makes a factory trial different from a lab screen?
A lab screen may indicate technical potential. A factory trial tests whether that potential survives real operating conditions and creates a measurable business case.
What happens after a successful application test?
The next step is usually a controlled production validation, extended run, or procurement qualification review. We help define the scale-up plan and decision gates before bulk supply is considered.